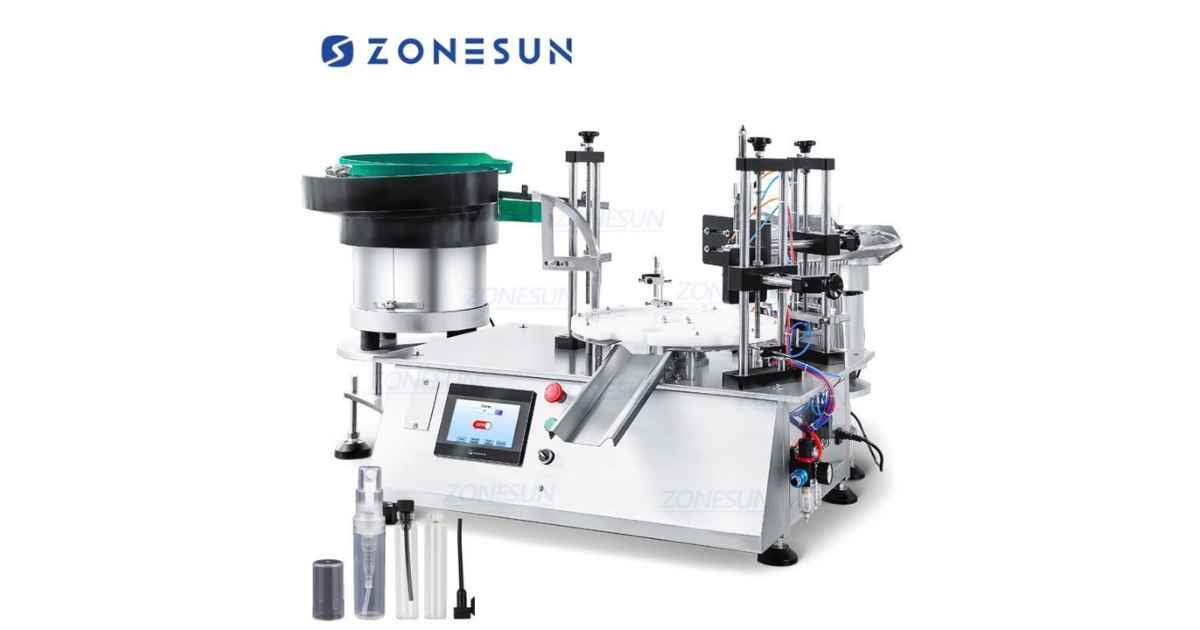
Modern packaging lines often combine several processes to improve efficiency and reduce manual handling. Monoblock filling machines are designed to combine multiple packaging operations within one integrated machine structure. Depending on the model, these operations can include rinsing, filling, capping, or other container-handling functions.
By combining processes into a compact system, monoblock equipment can help manufacturers save floor space and create a more streamlined production workflow.
What Are Monoblock Filling Machines?
A monoblock filling machine integrates two or more packaging processes into a single machine.
A conventional packaging line may use separate machines for different operations. A monoblock design brings multiple functions together, allowing containers to move directly from one stage to another within the same integrated system.
The exact configuration depends on the application. Some machines combine filling and capping, while others may include rinsing, filling, and capping.
How Monoblock Systems Work
Empty containers enter the machine through an infeed system. Depending on the configuration, containers may first pass through a rinsing or cleaning stage.
They then move directly to the filling section, where the required amount of product is dispensed.
After filling, containers can move immediately to a capping or sealing station. The finished containers are then transferred to an outlet conveyor for labeling, inspection, or further packaging.
The integrated design reduces the distance containers need to travel between individual operations.
Benefits of Monoblock Equipment
One major benefit is space efficiency. Combining several processes into one machine can reduce the floor area required compared with installing multiple independent machines.
Monoblock systems can also reduce the amount of container handling between stages. Fewer transfers can simplify the production process and potentially reduce handling-related issues.
Another advantage is coordinated operation. Since the different stations are mechanically and electronically integrated, their timing can be managed as part of one system.
Applications in Beverage Production
Monoblock filling systems are commonly used in beverage packaging applications.
Depending on the machine design, a beverage line may include container rinsing, filling, and capping within one integrated unit.
This can be useful for bottled water, juices, soft drinks, and other suitable liquid products.
The exact filling technology depends on the beverage characteristics and container type.
Food and Liquid Products
Food manufacturers can also use monoblock systems for suitable liquid products.
Products such as cooking oils, sauces, dressings, and other liquids may require different filling technologies depending on viscosity and product behavior.
A suitable monoblock system can combine filling with capping or other packaging operations, helping create a more organized production line.
Cosmetic and Personal Care Products
Cosmetic products often require controlled and clean filling processes. Monoblock machines can be configured for products such as lotions, shampoos, liquid soaps, and other personal-care formulations.
Product viscosity is an important factor when selecting the filling system. Thick products may require pumps or piston-based filling mechanisms rather than systems designed for free-flowing liquids.
Filling Accuracy
Consistent filling is important for product quality and production cost control.
Monoblock machines can use different filling technologies depending on the product. Volumetric, piston, gravity, pressure, and flow-meter-based systems are examples of technologies that may be incorporated into filling equipment.
The manufacturer should recommend the appropriate system based on the product characteristics and required filling volume.
Container Handling
Container handling is an important part of monoblock machine design.
The machine needs to move containers smoothly between different stations while maintaining proper positioning.
Container dimensions, shape, material, and neck design can all affect machine compatibility.
If a facility uses several bottle sizes, it should ask the manufacturer about changeover procedures and required tooling.
Automation and Controls
Modern monoblock filling machines can use PLC-based control systems and touchscreen interfaces.
These controls allow operators to monitor machine operation and adjust appropriate production parameters.
Sensors can monitor container presence, machine position, filling conditions, and other functions. Automated controls can also help coordinate the timing of different stations.
Hygiene and Cleaning
Hygiene is especially important when filling food, beverage, cosmetic, or pharmaceutical products.
Product-contact surfaces should be made from appropriate materials and designed to support cleaning.
Some systems can be configured for automated cleaning procedures, depending on the application.
Operators should follow the manufacturer’s cleaning instructions and the applicable hygiene requirements for the product being manufactured.
Maintenance Requirements
Regular maintenance helps keep monoblock equipment operating reliably.
Operators should inspect filling valves, pumps, conveyors, seals, sensors, capping mechanisms, and other components according to the manufacturer’s maintenance schedule.
Preventive maintenance can help identify worn components before they cause significant production interruptions.
Keeping spare parts available for critical components can also reduce downtime during maintenance.
Choosing the Right Monoblock Machine
Before purchasing a monoblock system, manufacturers should identify the product type, filling volume, container design, production capacity, and required packaging operations.
The machine’s dimensions and utility requirements should also be considered when planning the production area.
Businesses should discuss expected production growth with the manufacturer. A suitable system should ideally meet current requirements while providing a practical foundation for future production needs.
Conclusion
Monoblock filling machines combine multiple packaging operations into an integrated system, helping manufacturers streamline container handling and make efficient use of production space.
Depending on the design, a monoblock machine can combine processes such as rinsing, filling, and capping. These systems can be used in beverage, food, cosmetic, personal-care, and other liquid-product applications.
When selecting equipment, manufacturers should consider product characteristics, container compatibility, filling accuracy, production speed, hygiene, automation, maintenance, and future expansion.
With appropriate configuration and regular maintenance, monoblock filling equipment can support an efficient and organized packaging operation.
Disclaimer: The information provided in this article is for general informational and educational purposes only and does not constitute professional engineering, manufacturing, or regulatory advice. Equipment specifications, performance, and compliance requirements vary by manufacturer and application. Readers should consult qualified production engineers and regulatory professionals before selecting or installing any filling system. The author and publisher disclaim all liability for production issues, equipment failures, or financial losses arising from reliance on this content. Always verify hygiene standards, safety certifications, and local regulations before purchase.
Uncover solutions that stand up to scrutiny—dive into our evidence-backed content and act with certainty.